Table of Contents
Titanium Plate Tolerances: How Buyers Should Specify Thickness, Flatness, and Cut Size
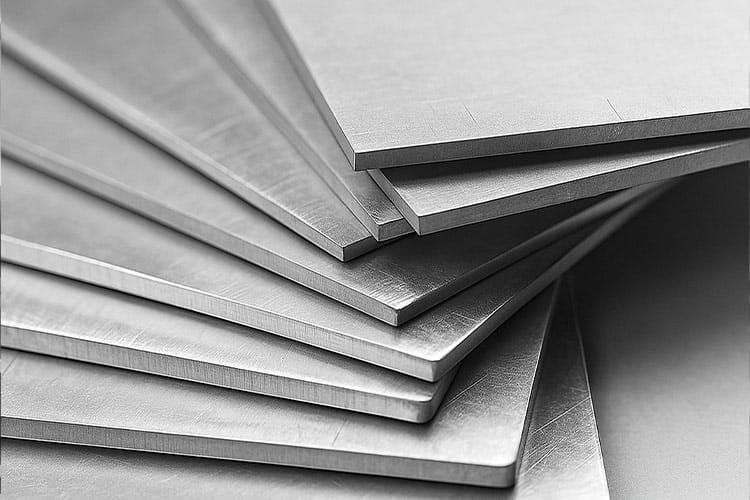
Titanium plate tolerances should reflect the supplied product standard, thickness range, plate size, cutting route, fabrication sequence, and finished-part requirement. Thickness, width, length, flatness, edge condition, and squareness describe different characteristics. A single “tight tolerance” note does not tell the supplier or receiving inspector what matters.
This guide helps industrial buyers specify mill plate and cut blanks without confusing raw-material tolerances with finished-machined dimensions.
Confirm whether the product is plate, sheet, or strip
Product terminology affects the applicable standard, normal dimensions, and tolerances. State the product form and specified standard rather than choosing a name from thickness alone. ASTM B265 covers titanium and titanium alloy strip, sheet, and plate within its scope.
Use the titanium plate and sheet specification guide to align grade, product form, condition, dimensions, and records before adding project-specific limits.
Specify thickness and its measurement basis
State nominal thickness, units, tolerance basis, and any required minimum thickness. A nominal dimension with plus-and-minus tolerance is not the same as a minimum-only requirement. Confirm whether measurements exclude edge zones or other locations under the governing specification.
If the plate will be machined on both faces, define the stock needed for cleanup and final geometry. Thickness tolerance does not create machining allowance unless the purchasing plan deliberately accounts for the full supplied range.
Define width, length, and cut-size tolerance
| Characteristic | Buyer decision | Inspection question |
|---|---|---|
| Thickness | Nominal, tolerance, and cleanup allowance | Where and how many readings are required? |
| Width and length | Mill size or cut blank | Are limits applied before or after edge finishing? |
| Squareness | Needed for nesting or direct fabrication | What datum and method will be used? |
| Flatness | Needed for fixturing, welding, or machining | What support condition and span apply? |
| Edge condition | Sheared, sawed, waterjet, machined, or deburred | Which edge features are acceptable? |
Cut blanks need their own tolerance and edge definition. Do not assume a mill plate tolerance automatically controls a waterjet or saw-cut blank. Identify the cutting route when it affects taper, heat-affected condition, burrs, or allowance.
State flatness with size and support conditions
Flatness depends on plate dimensions, thickness, residual stress, cutting, support, and measurement method. A plate resting under its own weight can show a different result from one measured on a controlled support arrangement. State the applicable standard or method and the area over which the limit applies.
ASME Y14.5 provides a recognized dimensioning and tolerancing framework for engineering drawings. The raw plate purchase order still needs a practical inspection definition suited to the supplied product.
Account for cutting and stress redistribution
Removing blanks from a larger plate can release residual stress and change flatness. Narrow strips, asymmetric shapes, and heavy material removal may move after cutting or machining. Buyers should distinguish incoming plate acceptance from blank acceptance and final-part acceptance.
If flatness after cutting is critical, discuss the cut sequence, blank geometry, intermediate stress management, machining plan, and inspection stage. Do not assign final-component flatness to untouched mill plate without a process basis.
Coordinate surface condition and dimensional allowance
Descaling, grinding, machining, and surface cleanup can change thickness. Specify the delivered condition and whether reported dimensions apply after surface preparation. The ASTM B600 guide addresses descaling and cleaning titanium surfaces; use project-specific acceptance requirements alongside it.
If cosmetic appearance matters, define it separately from thickness and flatness. A visually uniform surface can still be dimensionally nonconforming, while acceptable mill texture may disappear during machining.
Plan inspection coverage and reports
Define thickness measurement locations, width and length checks, flatness setup, edge inspection, sampling, and report format. Large plates may need a grid or mapped readings when local variation affects nesting or minimum finished thickness.
A material certificate reports material evidence required by the order; it does not automatically contain a complete dimensional map. Quality management certification such as ISO 9001 also does not replace shipment-specific inspection.
Avoid over-tolerancing stock plate
A machined component may need tight final dimensions while the parent plate only needs enough stock and flatness for stable setup. Adding finished-part limits to raw plate can force unnecessary grinding or machining before the buyer performs the same work again.
However, loose plate control can create setup, clamping, welding, or cleanup problems. Use the actual manufacturing route to decide which characteristics need tighter control and which can remain at the product-standard level.
Write a plate tolerance RFQ
- State grade, product form, standard, edition, and condition.
- List nominal thickness, width, length, and units.
- Define flatness, squareness, and edge condition only as needed.
- Separate mill plate limits from cut-blank and final-part limits.
- Provide machining allowance and critical minimum stock.
- Define inspection locations, sampling, reports, and traceability.
Review related material choices in the titanium plate grade guide. For a project review, send XFDY the plate specification, blank drawings, quantities, cutting route, and inspection requirements.
Plate tolerance decisions should be tested against the planned nesting and machining sequence. Mark critical blanks on the plate layout, identify the minimum finished thickness, and calculate how much stock must remain after flattening, surface cleanup, and machining. Large noncritical remnants do not need the same mapped inspection as areas assigned to thin finished features. This risk-based approach focuses measurement where material variation could prevent the required component geometry.
Define the inspection setup before requesting a flatness limit. Support spacing, plate orientation, measurement span, edge exclusion, temperature, and whether the plate is restrained can change the observed result. The ASME Y14.5 framework supports drawing tolerances, while raw plate acceptance also needs the relevant product standard and a practical method agreed with the supplier. Record the method on the RFQ or inspection plan when flatness is critical.
Coordinate plate requirements with the fabricator that will cut and machine the material. Thermal cutting, mechanical cutting, clamping, welding, and heavy one-sided machining may redistribute stress or introduce distortion after incoming inspection. Separate responsibility for as-supplied plate, cut blanks, welded assemblies, and finished parts. The titanium plate processing guide provides additional context for planning these stages.
For an initial order or a high-consequence application, consider an agreed thickness map and flatness record for representative plates. Specify the grid, edge offsets, instruments, reporting units, and acceptance logic. Once capability and incoming performance are understood, the sampling plan can be reviewed. Do not request an extensive report unless the data will be used for acceptance, nesting, or process planning.
The purchase order should bring these decisions together: grade, standard and edition, condition, nominal dimensions, applicable standard tolerances, any added project limits, measurement stage, reporting, marking, and protective packing. When a supplier proposes an alternative tolerance or inspection method, evaluate its effect on minimum stock and downstream setup before approval. This keeps plate procurement aligned with the real fabrication risk rather than an isolated numerical limit.
Conclusion
Useful titanium plate tolerances separate mill-product requirements from cut-blank and final-part requirements. Buyers should define measurement bases, account for cutting and machining, coordinate surface condition with allowance, and request only the inspection coverage needed for reliable fabrication.
FAQ
What tolerance applies to titanium plate thickness?
Use the specified product standard and edition, thickness range, plate dimensions, and condition. Add project-specific limits only when the fabrication or finished part requires them.
Is nominal thickness the same as minimum thickness?
No. Nominal thickness is subject to its stated tolerance, while a minimum requirement sets the lowest acceptable value. State the intended basis clearly.
Why can titanium plate move after cutting?
Cutting can redistribute residual stress, especially in narrow or asymmetric blanks. Evaluate flatness at the stage where it matters and plan the cutting and machining route.
Does mill plate flatness guarantee final-part flatness?
No. Cutting, clamping, welding, and machining can change geometry. Final-part acceptance needs its own drawing and process control.
Should every titanium plate receive a full dimensional map?
Not necessarily. Choose measurement coverage from product size, risk, minimum stock needs, fabrication method, and customer requirements.