جدول المحتويات
Titanium Bar Tolerances: How Buyers Should Specify Diameter, Straightness, and Length
Titanium bar tolerances should be selected from the finished-part geometry, machining route, workholding method, and applicable product standard. Tighter numbers are not automatically better. They can restrict supply and add inspection effort without improving the finished component if the first machining operation removes the relevant surface.
This guide helps buyers define bar diameter, ovality, straightness, length, and cut-end requirements for machining and fabrication. Final tolerances must be approved by the responsible engineering and quality teams for the application.
Begin with the product standard and bar condition
State the grade, bar shape, condition, and governing standard before adding drawing requirements. أستم B348/B348M covers titanium and titanium alloy bars and billets within its scope. Buyers should use the specified edition and review its dimensional and product requirements rather than applying a remembered tolerance from another material.
The supplied condition matters because a ground bar, rough-turned bar, and descaled bar may serve different starting operations. Use the دليل اختيار قضبان وقضبان التيتانيوم to establish grade, form, and machining context.
Set diameter tolerance from machining allowance
A bar ordered at the finished diameter leaves no planned stock for cleanup. A much larger bar increases material removal and cycle time. Define a parent diameter that covers the finished envelope, expected surface cleanup, workholding, and process variation.
Do not use tolerance to replace allowance. Diameter tolerance describes the permitted supplied size range; machining allowance is the intentional stock available for creating the finished surface. Both need to be stated or derived from a controlled plan.
Address ovality and local size variation
| مميزة | لماذا يهم | Practical review |
|---|---|---|
| Diameter range | Controls minimum and maximum parent size | Measure at agreed locations and orientations |
| Ovality | Affects chucking, centering, and cleanup | Clarify whether it is included in size tolerance |
| الاستقامة | Affects bar feeding, turning, and long shafts | State method, span, and acceptance basis |
| طول | Affects blank planning and facing allowance | Define fixed, random, or cut length |
| End condition | Affects datum creation and safe handling | State saw cut, faced, deburred, or other requirement |
A single caliper reading cannot characterize an entire bar. Define sampling locations and the instrument appropriate to the tolerance. If ovality has a separate functional limit, state it rather than assuming every supplier calculates it the same way.
Specify straightness with a clear method
Straightness requirements need a reference length and measurement method. A limit per unit length and a total-length limit answer different questions. Long bars for automatic feeding may need controls that are unnecessary for short blanks.
The drawing team should use established dimensioning principles. ASME Y14.5 provides a recognized framework for dimensioning and tolerancing, but the purchase order must still define the applicable measurement setup and acceptance requirement.
Choose full length or cut blanks intentionally
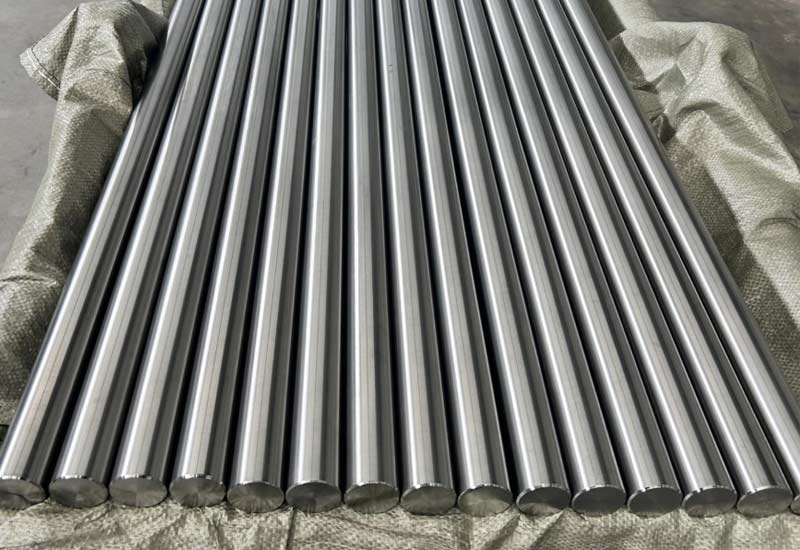
Full-length bars can support flexible nesting, while cut blanks reduce internal sawing. The correct choice depends on part mix, handling, traceability, and machining setup. For fixed blanks, include length tolerance, facing allowance, burr control, and squareness only where needed.
ال دليل قطع شريط التيتانيوم حسب الحجم explains how length, grade, tolerance, and lot identification should remain connected.
Do not over-tolerance nonfunctional stock surfaces
If the entire bar surface will be rough turned, a very tight supplied diameter may not improve the final part. It can reduce the number of available stock routes and add grinding or sorting. Reserve narrow limits for characteristics that protect machining, material utilization, or final conformance.
Conversely, loose stock control can be costly when the finished part has little cleanup allowance or when long, slender bars must run through guides. Document the process reason for each added requirement so suppliers can propose suitable material honestly.
Plan inspection and sampling before shipment
State which dimensions are reported, sample size, measuring equipment where relevant, and whether inspection records are required before release. A material certificate normally does not replace a dimensional report. Link reports to the delivered heat, lot, bundle, or blanks.
Quality-system certification such as ايزو 9001 does not define the bar tolerance or prove that the shipment meets it. Product-specific inspection is still required by the order.
Connect tolerance to surface condition
Diameter measurements can be influenced by scale, grinding marks, local defects, and the supplied surface condition. State whether the bar is descaled, ground, rough turned, or otherwise prepared, and define which visible conditions require review. The titanium bar surface finish guide covers this decision separately.
Write a usable bar tolerance RFQ
- Provide the finished-part drawing and identify the first machining operation.
- State grade, product standard, bar shape, and delivery condition.
- List diameter, ovality, straightness, length, and end requirements with units.
- Define machining allowance separately from supplied tolerances.
- State dimensional sampling and report requirements.
- Ask suppliers to identify every exception before acceptance.
Send XFDY the finished drawing, parent-bar requirement, quantity, and inspection plan for a manufacturability review. Include the intended bar feeder, workholding, or blanking method when it affects straightness or length.
A useful tolerance review begins with the machining setup. Long titanium bars may need straightness control because runout affects support, rotation, and tool engagement, while short sawn blanks may be governed mainly by diameter and available cleanup stock. Identify the length actually used in one setup and the minimum finished diameter after machining. This lets the buyer define incoming requirements from process needs instead of applying the tightest possible limit to every bar.
Measurement language must be practical. State whether diameter is checked at several positions and orientations, how out-of-roundness is derived, and whether straightness is evaluated as total indicator reading or by another agreed method. The ASME Y14.5 framework helps define engineering tolerances, but raw bar acceptance must also match the applicable product specification and the agreed inspection setup. Avoid copying a finished-part drawing tolerance directly onto mill bar without a manufacturing reason.
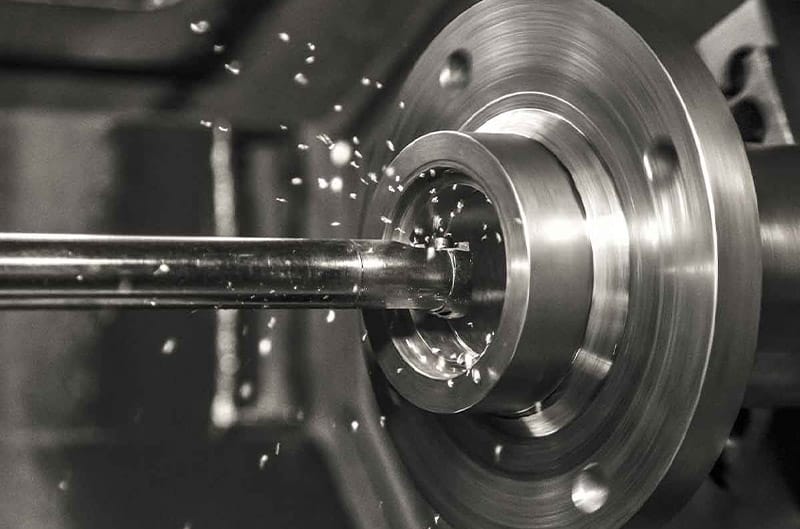
Allow for cutting, end condition, and handling. Sawed ends may require facing stock; chamfers or protective end treatment may matter for automated feeding; and long bars need supports that prevent damage or permanent bending during storage. When multiple cut lengths are ordered, identify the permissible length variation and whether remnants are acceptable. The titanium bar stock selection guide connects grade, size, condition, and machining route for buyer review.
For critical orders, request a dimensional report that reflects the agreed sampling plan and measurement locations. A report containing only one diameter value may not address taper, ovality, or local variation over a long bar. Conversely, a full map may be unnecessary for routine stock with adequate machining allowance. Align inspection effort with the consequence of insufficient cleanup, unstable setup, or assembly failure.
The final RFQ should distinguish standard product tolerances, any project-specific additions, and final-part requirements that remain the responsibility of the buyer. Ask the supplier to identify exceptions before order placement. This produces a titanium bar tolerance requirement that can be quoted, measured, and accepted consistently by both parties.
خاتمة
Effective titanium bar tolerances protect machining and acceptance without adding controls that provide no functional value. Start with the correct standard and condition, separate allowance from tolerance, define measurement methods, and align inspection with the actual production route.
الأسئلة الشائعة
What titanium bar tolerance should I specify?
Use the applicable product standard and add only the limits required by machining, workholding, material utilization, and finished-part requirements. There is no universal tolerance for every bar order.
Is bar ovality included in diameter tolerance?
That depends on the governing specification and order wording. If ovality has a separate functional limit, state the definition and measurement method explicitly.
How should titanium bar straightness be measured?
Define the support condition, measurement span, instrument or method, and whether the limit applies per unit length, total length, or both.
Should cut blanks have a tight length tolerance?
Only as tight as needed for facing allowance, workholding, material use, and downstream automation. Extra precision can add cost without improving the finished part.
Does a material certificate prove dimensional tolerance?
Usually not. A material certificate and dimensional inspection report serve different purposes. Request the report needed for the order.